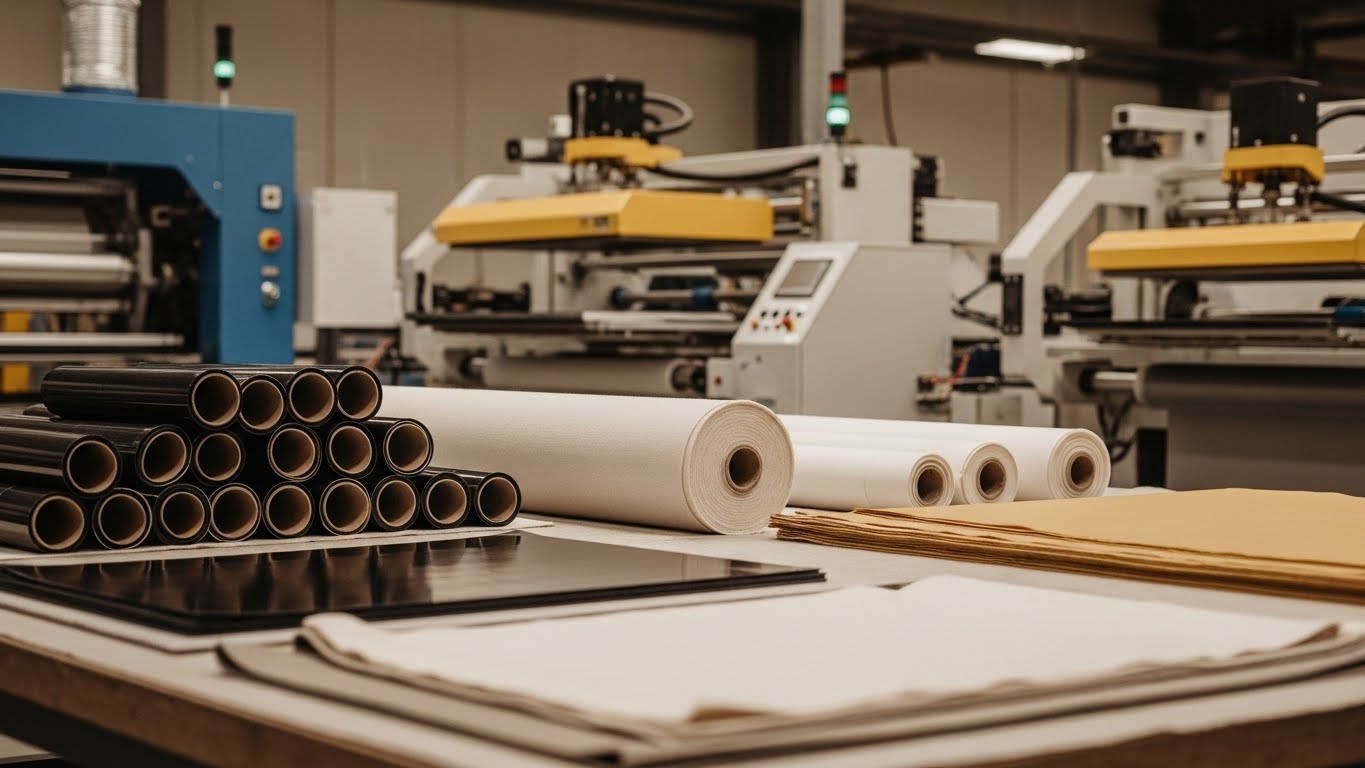
When a badge or embroidery lifts at the edge on apparel or sportswear, the cause is often the process window—not the artwork. Hotmelt BSN is a heat-activated, double-sided adhesive film used instead of stitching for a clean sew-free look. If heat, pressure, dwell and cooling are off, you get edge lift, incomplete bond or a stiff hand.
This guide shows what product and sourcing teams should lock at sample approval. Pair it with the material logic on the Hotmelt BSN film page and the wash durability guide when wash performance is in scope.
What to fix before you press
There is no universal heat-pressure-time recipe. Cotton, poly blends, elastane content and surface finishes respond differently on the same press. Start from the technical data sheet window, then confirm on your own line for each fabric family.
- Film thickness (micron): A thin badge and a thick epaulette do not need the same adhesive mass; too thick can squeeze-out, too thin can under-bond.
- Fabric moisture and surface: Damp or contaminated fabric weakens the bond; the press face must be dry and clean.
- Press calibration: Plate setpoint and real surface temperature often diverge; “the old setting” is unsafe without periodic checks.
- Cooling and peel: Early peel is a classic cause of edge lift; hot-peel versus cold-peel depends on the film grade.
Heat, pressure and dwell: a practical sequence
- Begin at the mid-point of the data-sheet window; do not jump to extremes on the first trial.
- Run three samples on the same fabric: midpoint, slightly lower heat, slightly shorter dwell. Compare appearance and edge hold side by side.
- Do not assume higher pressure always improves bond; excess pressure can crush the fabric or force adhesive sideways.
- Allow full cooling after the press, then peel as specified and inspect the edge.
- Lock the approved recipe on one sheet: fabric code, film micron, heat, pressure, dwell and peel type.
Common failures and what they usually mean
- Edge lift: Insufficient dwell, early peel or film–fabric mismatch.
- Centre bonds, edge fails: Uneven plate contact or pressure; large badge shapes may need better support.
- Stiff, plastic hand: Film too thick or heat too high; a thinner micron may suit that fibre.
- Wash failure: Visual sample approval is not enough—validate at the planned wash temperature and cycle count.
Hotmelt BSN uses a different bond mechanism from HF welding of TPU. It is meant for badges, embroidery backing and sew-free lines. If the same collection uses Premium TPU film with HF for logos and BSN for badges, keep the two recipes separate. When you move from sample to production lot, change one variable at a time so root-cause analysis stays possible.
Related solutions
This article was summarised and commented on by the LTS Frekans editorial team, drawing on the source article.